Inventory planning is the process of deciding what stock to carry, how much to keep, and when to reorder it. Its goal is straightforward: meet demand without tying up unnecessary cash in excess inventory. For UK manufacturers, that balance sits at the centre of daily operations. Too little stock and production stalls, orders slip, and customers look elsewhere. Too much and cash disappears into shelves and racking, obsolescence creeps in, and warehouse space fills with material nobody asked for.
This guide sets out the core inputs of good planning, the difference between planning and control, the methods most manufacturers use, and why the whole process needs regular review rather than a one-off calculation.
What inventory planning actually involves
Inventory planning sits ahead of the day-to-day work of moving goods. It looks forward and asks what the business will need, in what quantity, and by when. That covers raw materials, components, sub-assemblies, and finished goods. Each category has its own logic. A long-lead electronics component behaves very differently from a bag of flour that arrives next week.
Material Requirements Planning, usually shortened to MRP, is the system most manufacturers turn to for this. MRP is a computer-based approach to inventory management and production scheduling, designed to work out the raw materials and components needed to fulfil orders. It connects demand to supply in a structured way, rather than leaving planners to guess from spreadsheets and memory.
Planning affects more than the warehouse. It shapes production schedules, purchasing decisions, delivery promises, and the working capital tied up in stock. A manufacturer that plans well can quote confidently and produce without firefighting. One that plans badly spends its week chasing shortages.
The four inputs that drive every inventory plan
Good inventory planning depends on four main inputs. Get these roughly right and the plan is useful even if it is imperfect. Get them wrong and no software will save the result.
-
Expected demand. What customers will order, based on historical patterns, confirmed sales orders, and any forward visibility the sales team holds.
-
Available inventory. What is genuinely free to use, not simply what is sitting somewhere in the building.
-
Replenishment lead times. How long it takes to obtain more, from raising a purchase order to material arriving, inspecting, and being available for production.
-
Desired service level. The target for how often stock is available when needed, which directly dictates how much safety stock is sensible.
Each input carries uncertainty. Demand forecasts are rarely exact, supplier lead times drift, and stock records are not always accurate. A sound plan acknowledges this and builds in buffers where the risk justifies it, rather than pretending certainty exists.
Planning versus inventory control
Inventory planning and inventory control are different but closely connected, and mixing them up causes problems. Planning looks ahead and determines future stock needs. Control keeps current stock quantities and locations accurate right now.
Control is the record-keeping side: goods receipts, issues, stock levels, and where each item physically sits. Planning takes those records and turns them into decisions about replenishment. If control is weak, planning is built on sand. A plan generated from inaccurate stock records will produce either unnecessary purchase orders or unexpected shortages, and the planner will waste time second-guessing the system.
The two disciplines therefore reinforce each other. Book in goods promptly, record issues accurately, count stock regularly, and the planning function has something reliable to work with.
Why accurate availability data matters
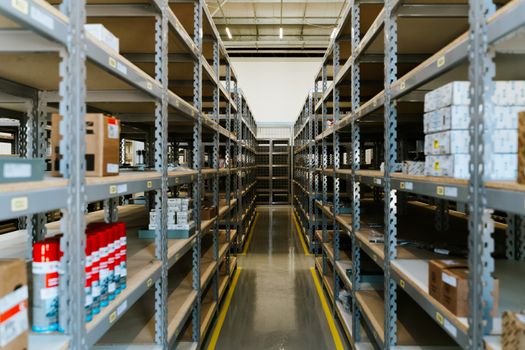
Accurate availability data is essential. Planning should account for stock on hand, allocated inventory, incoming orders, and safety stock rather than relying only on physical stock counts. This is one of the most common weak points in manufacturing businesses running on spreadsheets.
Consider a simple example. A warehouse holds 500 units of a component, so a physical count says 500 are available. But 300 are already allocated to a confirmed job and 50 are held as safety stock. The genuinely available figure is 150. A planner working from the physical count will under-order, then discover the problem too late.
Systems that distinguish between on-hand, allocated, and available quantities prevent this. So does discipline in how orders are entered and how allocations are maintained.
Reorder points and safety stock
Reorder points and safety stock help protect against uncertainty. A reorder point is the stock level that triggers a new order. Done properly, it accounts for expected demand during lead time as well as variability in demand and supplier performance.
The calculation has two parts. First, the demand expected while waiting for replenishment. Second, a buffer for the fact that both demand and lead time can move. A supplier who usually delivers in two weeks but sometimes takes four needs a different buffer than one who is consistently reliable.
Safety stock is not a sign of poor planning. It is a deliberate, costed decision about the level of risk the business is willing to accept. Setting it too low produces stockouts and expedited freight. Setting it too high ties up cash and storage. The right answer depends on the item, the customer, and the consequences of being short.
Common inventory planning methods
Several methods are in everyday use, and most manufacturers end up blending more than one. The right approach depends on demand predictability, product complexity, supplier reliability, and the type of business.
|
Method |
How it works |
Best suited to |
|---|---|---|
|
Reorder point planning |
Stock is replenished when it falls to a set level, calculated from demand during lead time plus a buffer. |
Stable, repeatable items with predictable usage. |
|
MRP |
Calculates material and component requirements from demand, bills of materials, and current inventory. |
Manufacturers with multi-level products and varied lead times. |
|
Just in Time (JIT) |
Material arrives close to when it is needed, minimising stock held. |
Reliable suppliers and predictable production flows. |
|
ABC analysis |
Items are grouped by value or importance, with tighter control on the highest-ranked items. |
Businesses with large and varied stock ranges. |
JIT is often discussed as though it were universally superior. In practice it demands dependable suppliers and steady demand. Where either is shaky, a JIT approach can leave production exposed. Many UK manufacturers adopt it selectively for specific commodity items while keeping buffers elsewhere.
ABC analysis is a useful sorting mechanism rather than a complete planning method. It helps focus attention where the money is, so that high-value items receive careful forecasting and low-value consumables get simpler rules.
Where MRP fits alongside ERP
MRP is the engine that works out what materials are needed. ERP software goes wider, offering inventory and stock management alongside shipping, purchasing, and product costing. In practice, the two are closely related. A manufacturing ERP typically contains MRP functionality, which is why the terms sometimes get used interchangeably in conversation.
MRP II extends the idea further. It checks routing details, setup and run times, labour standards, and machine availability to determine whether a job can realistically be completed on schedule. That shift from materials to capacity is what distinguishes MRP II from basic MRP.
For a growing manufacturer, the practical question is less about labels and more about whether the system gives planners a live view of inventory, demand, and capacity in one place. When inventory and MRP live inside the same ERP, the physical movement of goods and the financial value of that stock stay connected, which reduces reconciliation work at month end.
Making planning an ongoing process
Inventory plans need regular review. Demand, supplier lead times, inventory accuracy, and reorder parameters all change, so planning works best as an ongoing process rather than a one-time calculation. A reorder point set two years ago may be badly wrong today, particularly if the supplier base or product range has shifted.
A sensible review rhythm includes checking forecast accuracy against what actually happened, monitoring supplier performance against quoted lead times, verifying stock record accuracy, and revisiting safety stock levels for critical items. Seasonal businesses should adjust for known peaks rather than waiting for them to arrive.
It also helps to review exceptions rather than everything. Most planners cannot examine every part number each week. Systems that highlight items below reorder point, overdue purchase orders, or demand that exceeds forecast direct attention to where it is needed.
Getting the foundations right
Before investing in new software, it is worth checking the basics. Are bills of materials accurate and complete? Are lead times recorded against suppliers and items? Is stock counted with reasonable frequency? Is there a clear owner for the planning process? These foundations matter more than any feature list.
Where a manufacturer is moving from spreadsheets or a legacy accounting system, the transition to structured MRP usually starts with cleaning item data, defining reorder rules, and agreeing how demand enters the system. That groundwork is unglamorous but determines whether the software delivers anything useful.
Inventory planning rewards consistency more than sophistication. A simple process, applied reliably and reviewed honestly, will outperform an elaborate model fed with poor data every time.
Frequently Asked Questions
What is the difference between inventory planning and inventory control?
Inventory planning looks ahead and decides what stock will be needed in future, in what quantity, and when to reorder. Inventory control keeps current quantities and locations accurate through goods receipts, issues, and stock counts. The two depend on each other, because planning built on inaccurate stock records will produce the wrong replenishment decisions.
What are the four main inputs to inventory planning?
Good planning depends on expected demand, available inventory, replenishment lead times, and the desired service level. Each of these carries uncertainty, which is why buffers and safety stock exist. If any one of the four is significantly wrong, the resulting plan will either leave the business short of material or holding more stock than it needs.
How does MRP differ from reorder point planning?
Reorder point planning replenishes an item when stock falls to a set level, which suits stable, repeatable demand. MRP calculates requirements from demand, bills of materials, and current inventory, so it can handle multi-level products and varied lead times. Many manufacturers use both, applying reorder points to simple consumables and MRP to complex assemblies.
Is safety stock a sign of poor planning?
No. Safety stock is a deliberate decision about the level of risk a business accepts. Setting it too low produces stockouts and emergency freight, while setting it too high ties up cash and storage space. The right level depends on the item, the customer, and the consequences of being unable to supply.
How often should inventory plans be reviewed?
Plans should be reviewed regularly rather than treated as fixed. Demand, supplier lead times, stock accuracy, and reorder parameters all change over time. A practical rhythm involves checking forecast accuracy, monitoring supplier performance, verifying stock records, and revisiting safety stock for critical items, with extra attention during known seasonal peaks.
Free for 15 days, extendable to 30 by completing the guided onboarding. No credit card needed.
Click here for your free 15 day MRPeasy trial
Recent Comments